Beef Processor Improves Drainage Reliability with WSP™ Sludge Pump

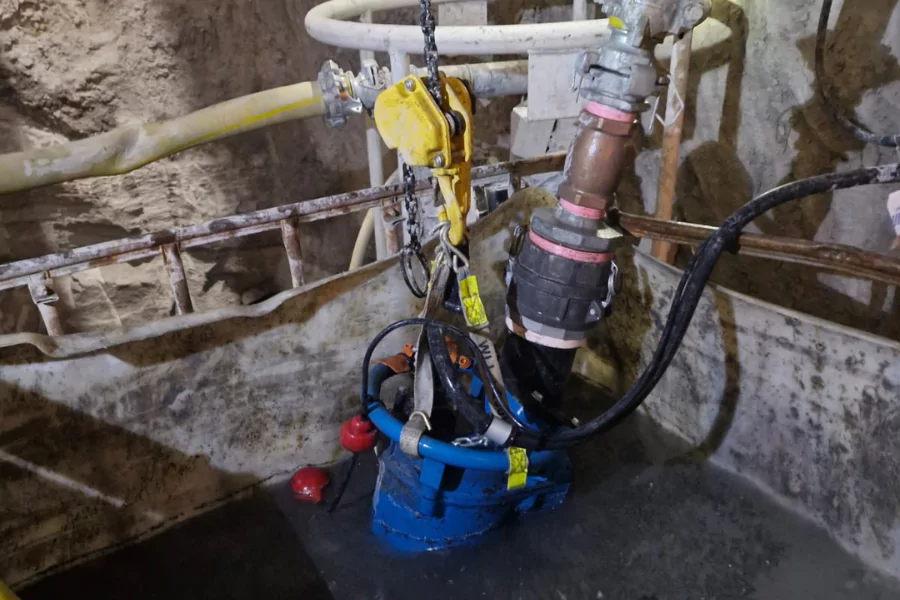
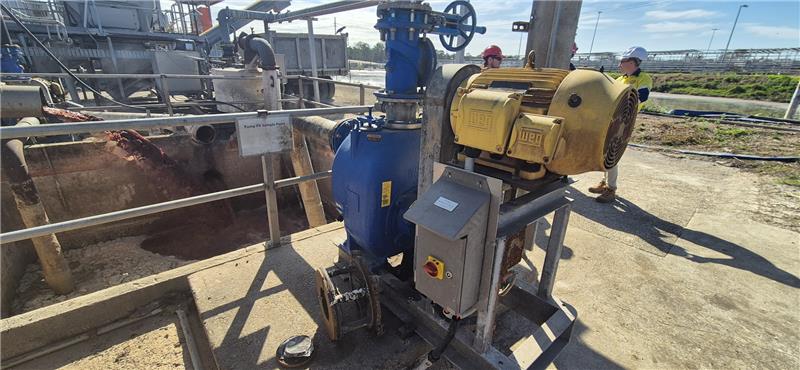
The Challenge In food processing, drainage systems face some of the toughest pumping conditions. At a beef processor, the tripe cook room’s drainage pit handled a mixture of fat, grass, small bone, grain, tripe offcuts, and hot water. Their existing pump struggled with the load, leading to frequent blockages, costly breakdowns, and high maintenance demands.

Beef Processor Improves Drainage Reliability with WSP™ Sludge Pump Read More »
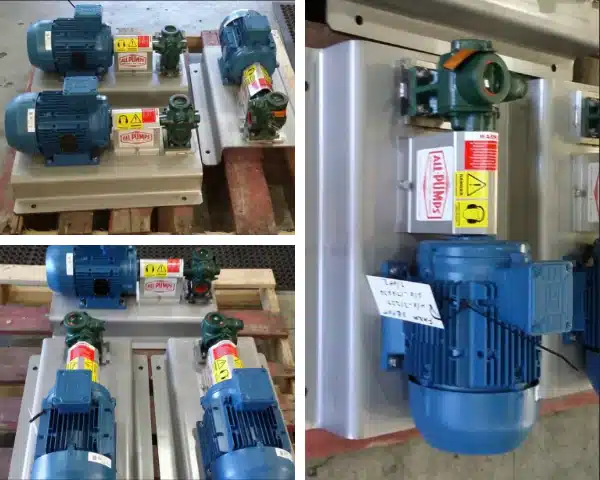
FTI Mag Drive Pump: Safe Acid Handling

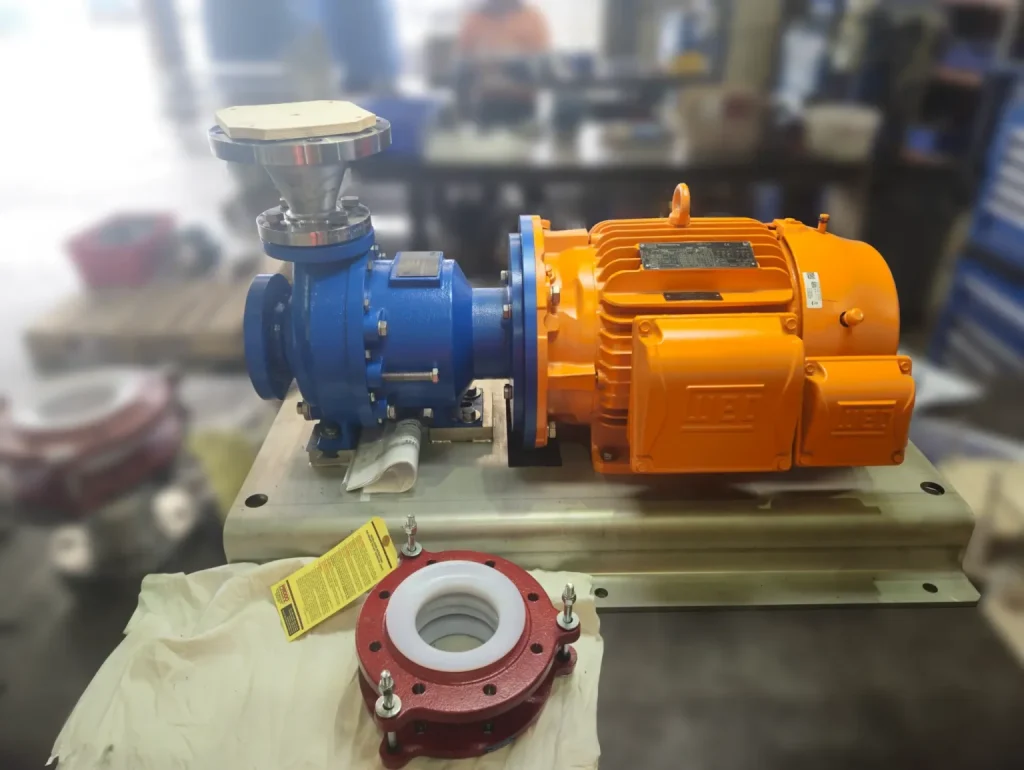
Problem A client required a replacement for their existing magnetic drive pump used for transferring 98.5% sulfuric acid. Given the hazardous nature of the acid, ensuring safe handling and protecting the equipment were critical considerations. Additionally, the client needed expansion joints for a 4-inch pipeline connection. Solution We supplied a Finish Thompson magnetic drive pump

FTI Mag Drive Pump: Safe Acid Handling Read More »

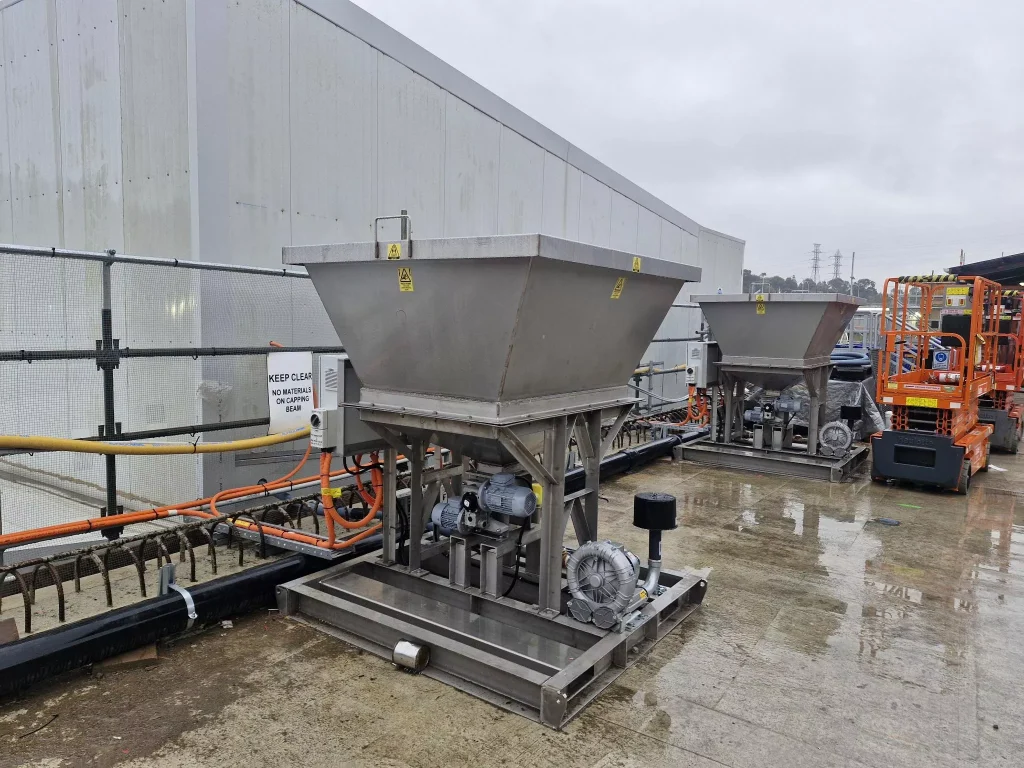
Large gray hopper unit beside an industrial building

Reliable Powder Dosing for Tunnel Construction

Overview All-Pumps supplied a compact, skid-mounted system that reliably meters dry polymer into a TBM conveyor process. The package integrates a micro-batch screw feeder and a side channel blower on a heavy-duty PFC base frame, with dedicated VSDs for easy adjustment of feed rate and airflow. The pre-assembled design simplifies installation and provides accurate, consistent

Reliable Powder Dosing for Tunnel Construction Read More »

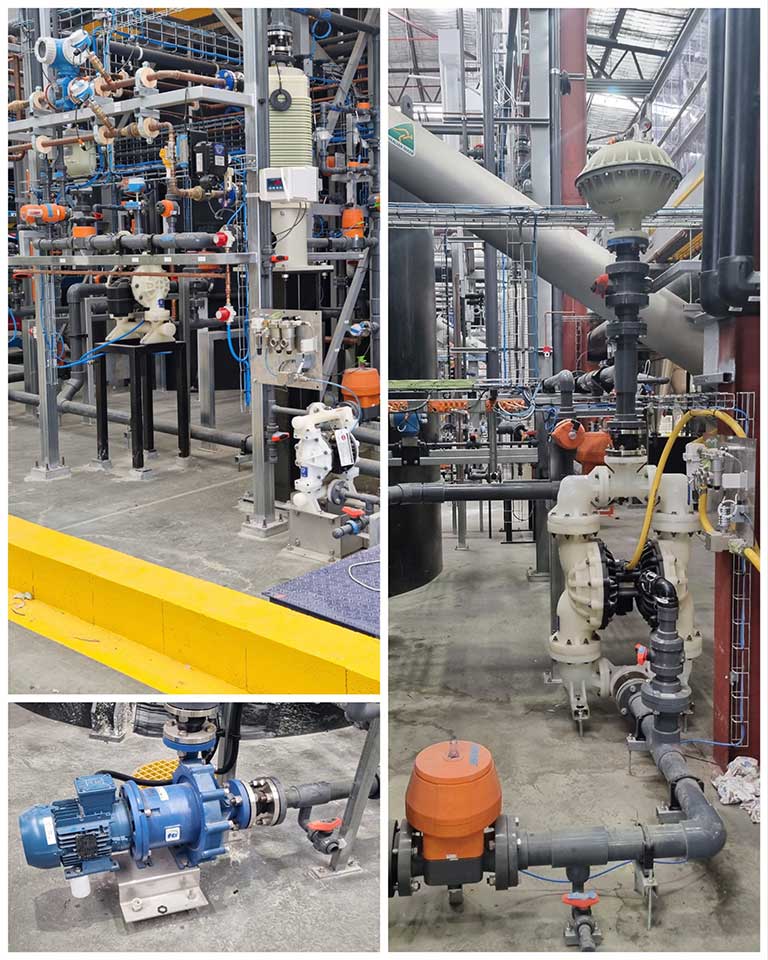
Industrial chemical pumps installed in a plant

Urban Mining Project

Problem A bio mining company needed large air-operated diaphragm pumps to build a new wet crush processing plant. Some of the chemicals they were pumping were highly corrosive and abrasive. They were a newish company and really needed to minimise capital outlay but still looking for reliable results. They also needed local support and knowledgeable

Urban Mining Project Read More »

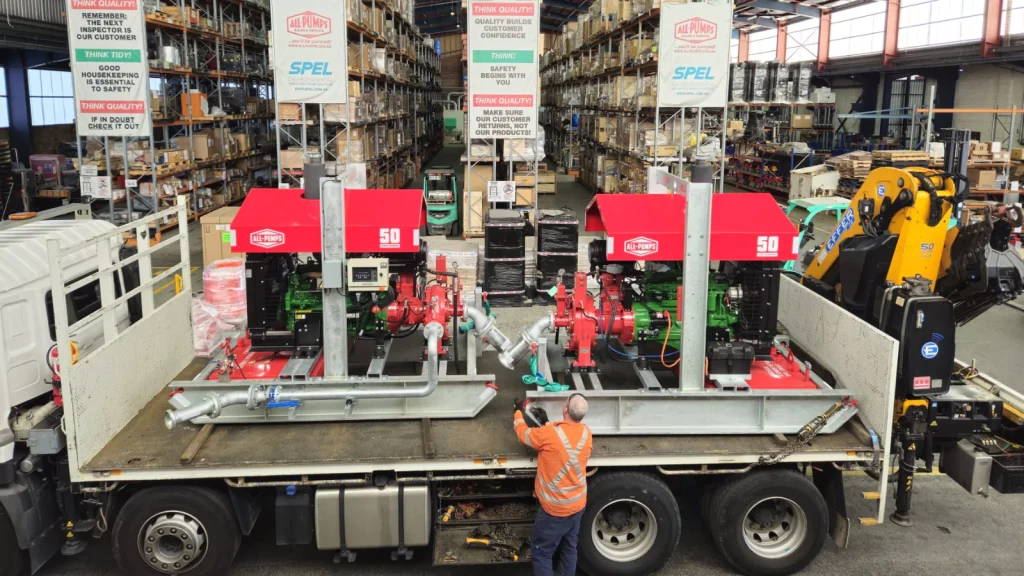
Red custom dewatering pump units in a workshop

Custom High-Head Dewatering Pump Sets for Ash Treatment

Problem A large energy company required two large turnkey dewatering pumps as part of an upgrade to their ash treatment process. Solution All-Pumps designed and delivered two custom drag skids with large-capacity, diesel-powered dewatering pumps. Each pump set was custom-built with a remote control, providing superior duty. Project Highlights Our team customised two Global Pump

Custom High-Head Dewatering Pump Sets for Ash Treatment Read More »

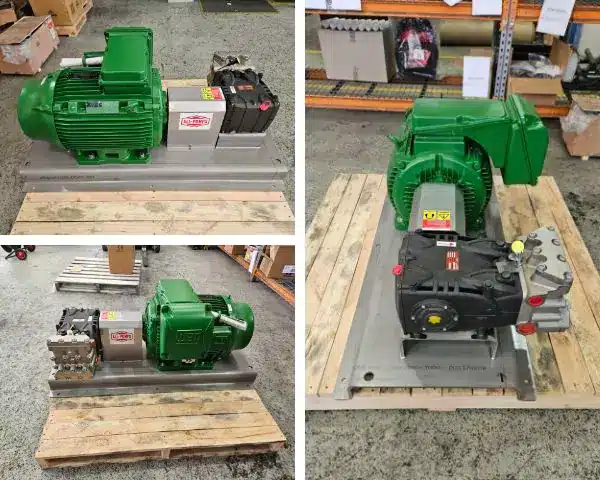
Corrosion-Resistant High-Pressure Pump Packages for Aggressive Chemicals

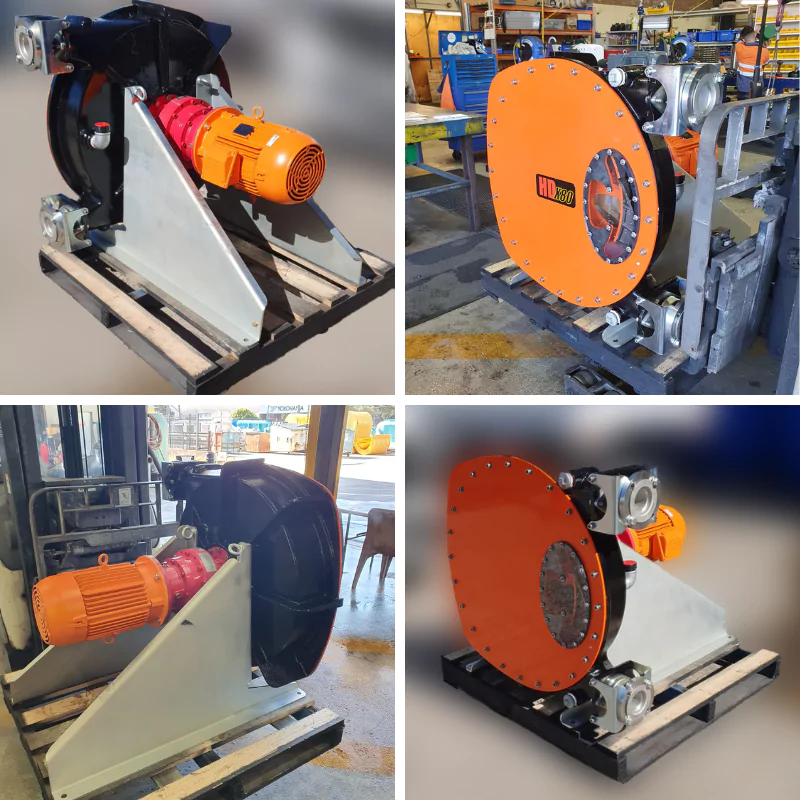
Overview All-Pumps built a complete pump package for an industrial process consultant that required a reliable solution for handling aggressive chemicals at high operating pressures. We handpicked a high-pressure plunger pump that meets the client’s requirements, coupled it with an industrial-grade motor, and assembled the components on a custom baseplate. Problem An industrial process consultant

Corrosion-Resistant High-Pressure Pump Packages for Aggressive Chemicals Read More »

Two tall yellow Tsurumi mine dewatering pumps

1000 Volt Dewatering Pumps Supplied to Mine Site

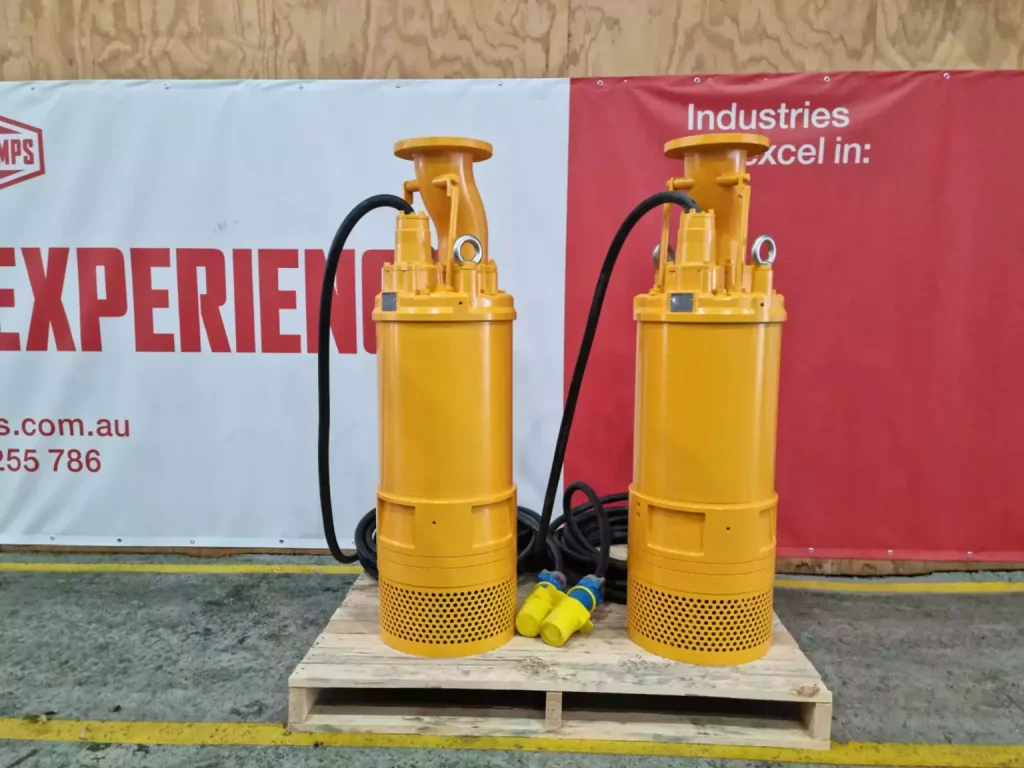
Problem An underground mine needed 1000-volt submersible pumps to dewater a sump on its site. Challenges included a unique duty and the immediate delivery of the pumps. Solution All-Pumps recommended Tsurumi LH619 submersible pumps to match the application’s unique flow and head parameters. Being an authorised Tsurumi distributor, we swiftly delivered the pumps to the

1000 Volt Dewatering Pumps Supplied to Mine Site Read More »

Shopping Cart
Scroll to Top