Cemo Pumps
CEMO Pumps (Pty) Ltd is a manufacturing company offering one of the most comprehensive ranges of pump types in Africa. The company was formed in 1957 as the Crown Group of Companies (Pty) Ltd and has supplied pumps and spare parts to both African and international markets for over 50 years.
CEMO manufactures a wide range of pumping technologies for demanding industrial applications. The company’s manufacturing facility is located in Johannesburg, covering more than 20,000 m² and incorporating:
- Machine shops
- Fabrication and assembly areas
- Foundry facilities
- Stores and inventory areas
- Pump testing facilities
All pumps and spare parts are manufactured in-house, allowing CEMO to maintain strict quality control while offering competitive pricing and realistic delivery timeframes.
Manufacturing Capabilities
CEMO’s manufacturing capabilities include a wide range of modern machining and fabrication technologies and specialize in the manufacturing of Helical Rotor Pump Solutions. They have their own in house quality control for both Stator and Rotor Manufacturing ensuring the geometry of both items match perfectly. This is a critical part of the quality of any helical rotor solutions.
CEMO Pumps operates under an ISO 9001:2015 internationally recognised quality management system, ensuring consistent manufacturing standards and product reliability.
CEMO Pumps specialises in the design and manufacture of several pump types commonly used in mining and heavy industrial environments:
Helical Rotor (Progressive Cavity) Pumps
The CEMO progressive cavity, positive-displacement pump is one of the most versatile designs on the market. Applications include Agricultural, Mining, Manufacturing, Waste-water, Water Utilities, Chemical, Petroleum and general industry fluid transfer. Our industrial range includes the SP (Small Pump), WDS (Widethroat), CB (Close-Coupled), O (Industrial), and HP (High Pressure) Ranges. Our extensive range of CEMO Pumps deliver flow rates up to 200m3/hr and pressures of up to 720m. A full service backup capability and comprehensive range of spares support all products.
- SP – Range
- WDS – Range
- O – Range
- HP – Range
Helical Rotor Borehole Pumps
High-Pressure Triplex Plunger Pumps
high pressure CROWN brand of triplex and Quintuplex pump ranges are perfect for use on underground and mining opencast operations. The CROWN brand of 707 high pressure and ultra-high pressure pumps are used extensively in concrete demolition, removal of graffiti, descaling of marine equipment and micro-hydro-power mining systems. These pumps are also used extensively in reverse osmosis plants as well as plate descaling in the steel mill industry.
The CROWN 350 medium to high pressure triplex pump has become a standard within the South African and North and South American mining operations. Its ability to operate at pressures of up to 20 MPa and with flows ranging from 130 – 210 l/min have made this the industry’s first choice for water jetting, general descaling, plant cleaning as well as micro-hydro-power mining systems which include rock drills, roof bolters, and rock and ore loaders which would have previously been powered pneumatically.
The CROWN 250 triplex high pressure pump is a compact version of the robust Crown 350. These are used primarily on municipal drain cleaning and honey-sucker type equipment used for unblocking sewer lines as well as drain cleaning. These are also used in the coal mining industry as a high pressure pump used in conjunction with a scrubber for dust suppression. Their compact size and light weight have made the CROWN 250 the preferred mobile, trailer mounted, diesel driven high pressure pump for building contractors, fire-fighters, plumbers and plant excavators. Pressures of up to 25 MPa and flows of up to 150 l/min are achievable with this all nodular iron and steel construction.
Crown 120 and Crown 737 are an underground industrial standard known for their /mud pumping abilities with SG’s of up to 1.15. The high flow (up to 44m3/hr) and high pressures (up to 225 bar) achievable on these pumps are what make them perfect for underground mine mud transfer as well as sewage plant sludge movement. These pumps are also extensively used in steel mill plate descaling, mud drilling and for pumping light tar’s and resins within the petro-chemical industry.
Materials of construction include fabricated steel casings with bronze crosshead wear liners, nodular iron eccentric and connecting rods transferring the fluid via steel, thermally coated plungers through forged steel fluid ends. Eccentric drive is via heat treated jackshaft pinions on eccentric ring gears. The pumps recommended slow eccentric speed (120 rpm) ensures pump reliability and wear component longevity.
High-Flow Multistage Centrifugal Pumps
The Cemo highly efficient multistage pumps are manufactured with the highest grade of certified materials and ultra-precise machining. The Clearwater range includes our CPH 480, CPH 505, CPH 530, CPH 540 and our CPH 580 pumps. These high flow (415 m3/hr – 888 m3/hr) pumps can be used with a range of pressures provided by the number of stages in series. (Up to 120 Bar.)
Materials of construction are sand and die cast PB1 Phosphor bronze impellers, diffusers, shaft sleeves, neck rings, neck bushes, balance and counter disc components. All stage casings, suction and delivery covers are cast from A-2 Steel or Gr17 Cast Iron or SG42 nodular iron as per customer’s requirements. Anti-abrasive coatings such as HVOF tungsten carbide, ceramic coatings and chrome plated coatings are used on wear susceptible wetted components or rotating element assemblies.
All rotating element individual components and assemblies are balanced to ISO 19401 prior to assembly. All pump shafts are non-destructively tested and heat-treated to relieve residual stresses. Pump bearing types include either white metal shell types or branded roller bearing types dependent on pump type and model.
We also refurbish various other OEM multistage type pumps with our extremely high quality machined components which are interchangeable with these pumps, as well as innovative hydraulic improvements for enhanced pump performance and efficiencies. Independent test results showing improvements are available on request.
Our in house foundry and all on site machining undertaken on our premises ensures speedy delivery of a quality engineered product. All processes follow our accredited ISO 9001:2008 quality standard. Independent pump testing is carried out at the South African Bureau of Standards (SABS) and all pumps are tested to ISO 9906:2012 Grade 1 standards unless otherwise specified by client.
On site commissioning and pump condition monitoring are carried out b y our field service engineers and technicians who are available 24 hours/day, 7 days a week for commissioning and breakdown services. On-site pump repairs to wear faces, balance valve assemblies are also carried out by the same team of pump experts. Pump condition monitoring is also a service offered by our pump field service team on either a monthly or fixed periodic basis. Monitoring includes pump flow readings, pressure readings, energy consumption and overall efficiency.
Mobile Dewatering System for Mining
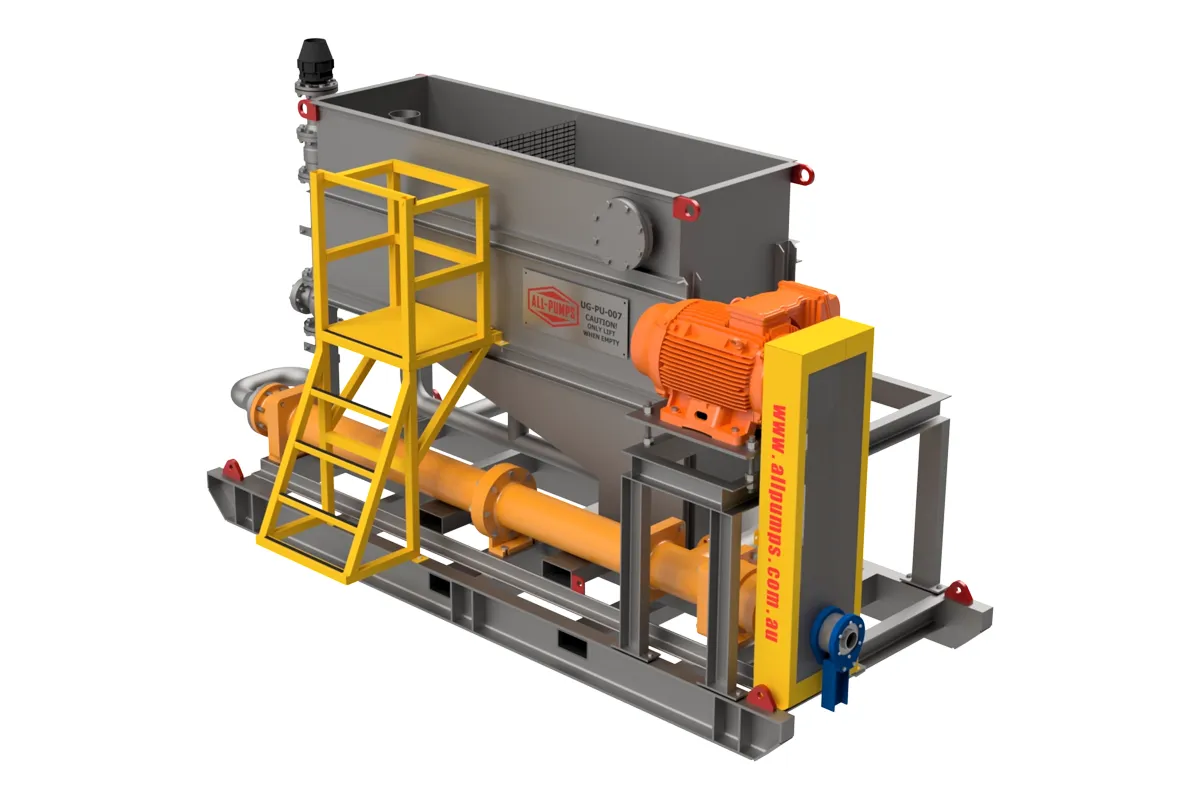
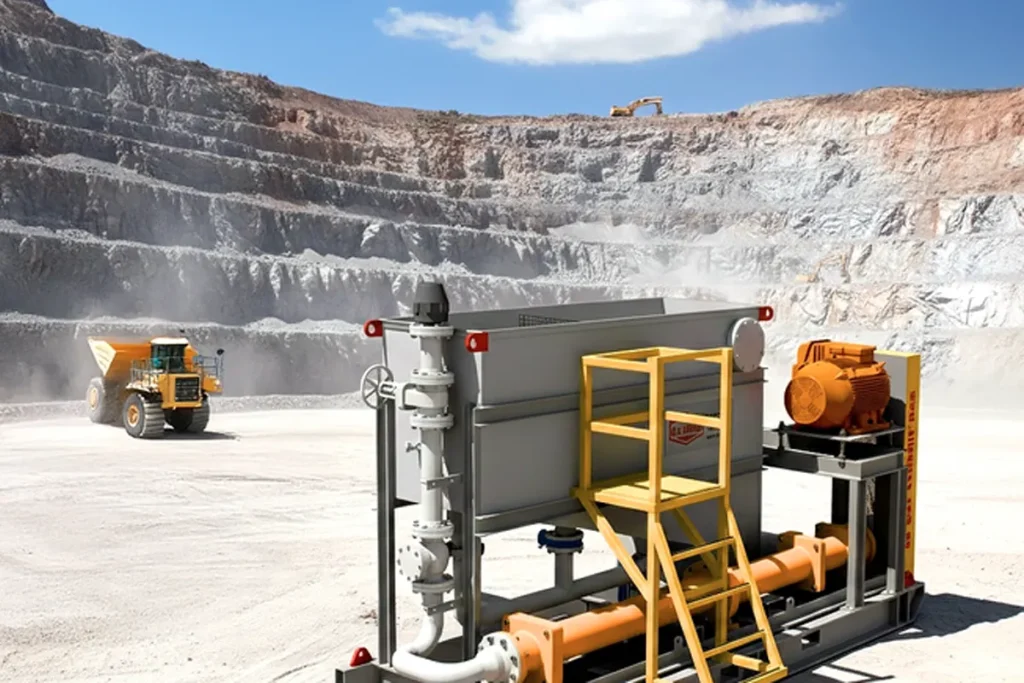
All Pumps “Fish Tank” Mobile Dewatering System is designed to provide dependable mine dewatering performance in demanding field conditions. Built for mobility, durability, and ease of maintenance, the system helps mining operations manage water efficiently while minimizing downtime.
Features & Benefits
- Dewatering Tank: Dewatering Tank improves slurry handling and separation of large solids.
- Stainless Steel End Covers, Clamp Plates, and Stator Stainless Steel End Covers, Clamp Plates, and Stator for extended service life in saline and harsh mine water conditions.
- Maintenance-Free Flexible Drive Shaft No pins or wearing rubber sleeves
- Internal Anti-Reverse Clutch These are available on Mark 1 Models and stop back flow
- Easy Repair Stator Clamps Much easier to work on than pumps with long connecting rods that hold the pump together. They have proven to be more reliable under pressure in highly corrosive environments.
- Reliable Belt Drive System Over-engineered and highest quality belts are used to minimize downtime. All systems leave our factory laser-aligned.
- Pump Transfer Cradle Suitable for removing the pump only when rotating a pump for maintenance, underground minimizing downtime.
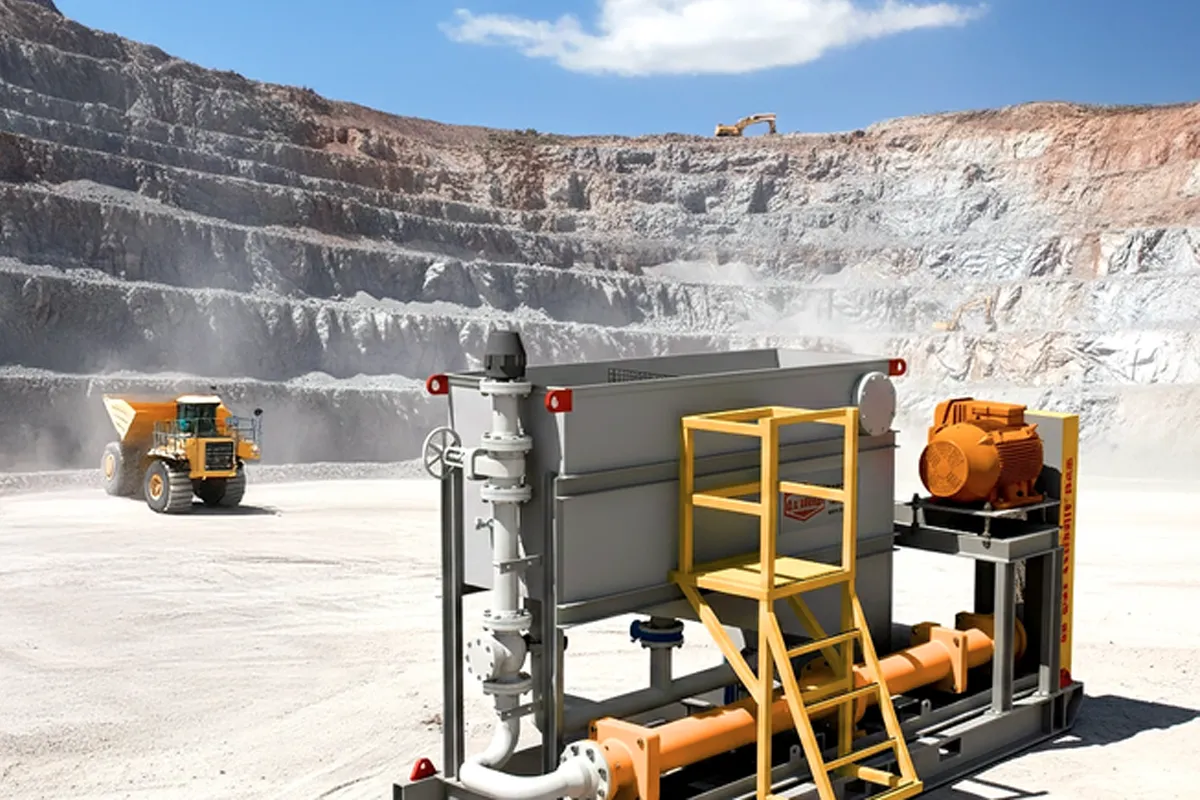
Open Pit Transfer Pump Station Application
In open pit mining operations, reliable transfer pumping is essential for moving slurry, water, and process fluids across long distances. CEMO pump systems are designed to handle abrasive solids, fluctuating flow conditions, and demanding site environments while maintaining consistent performance.
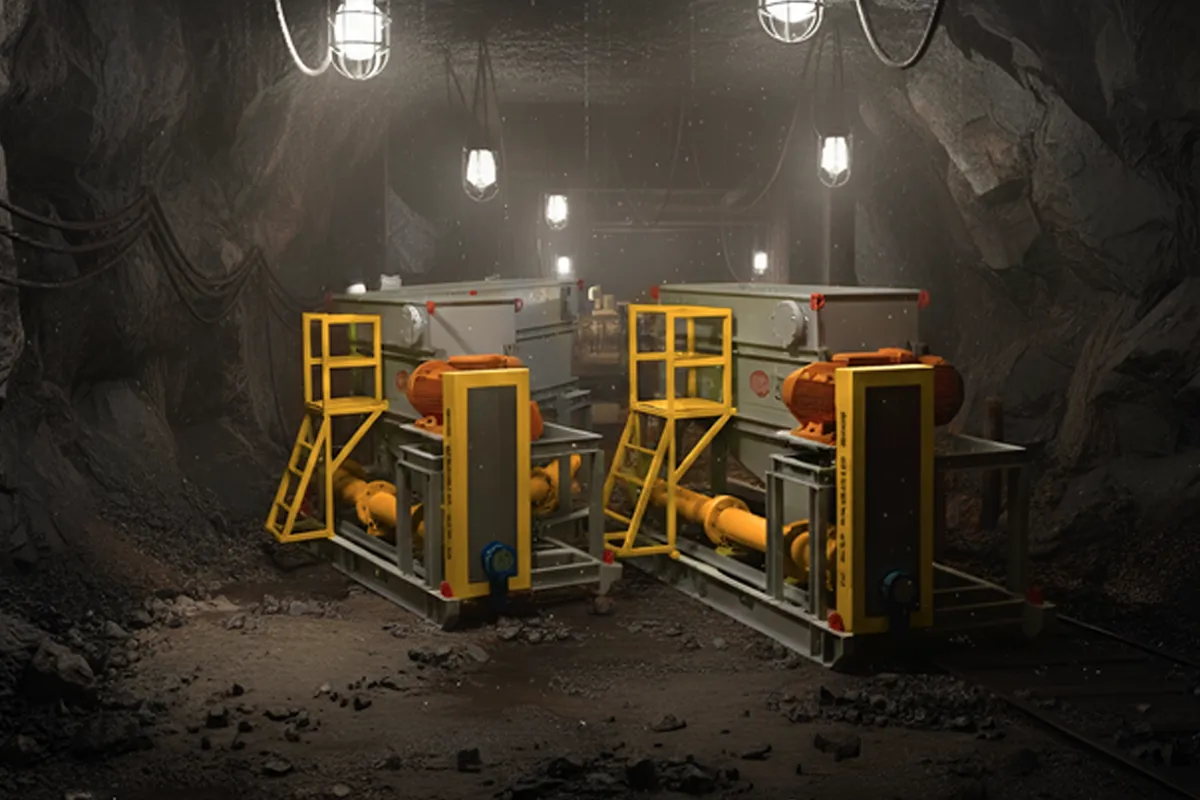
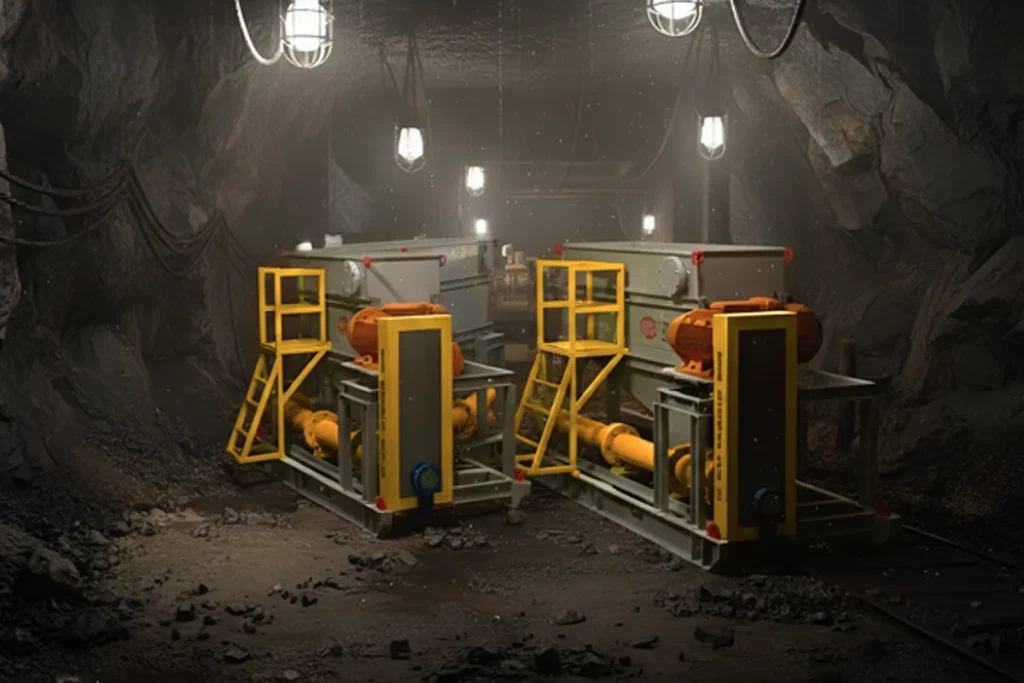
Underground Mining Application
Underground mining environments require compact, durable pumping solutions capable of operating reliably in confined and challenging conditions. CEMO pump systems support critical underground operations such as dewatering, slurry transfer, and process fluid handling, helping maintain safe and efficient mine operations.
They have proven to be the lowest cost dewatering for underground mining where flows of 100 liters per second or lower are experienced with high discharge head pressures.